Fe and NFe are two different measurements
On steel the gauge uses magnetic induction. The probe generates a magnetic field, the steel underneath responds, and the strength of that response varies with how far away the steel is, which is the coating thickness. That is the Fe mode.
On aluminium, copper and other non-ferrous metals there is no magnetic response to measure, so the gauge switches to eddy current instead. It induces small circulating currents in the metal and measures their effect, which again varies with distance. That is the NFe mode.
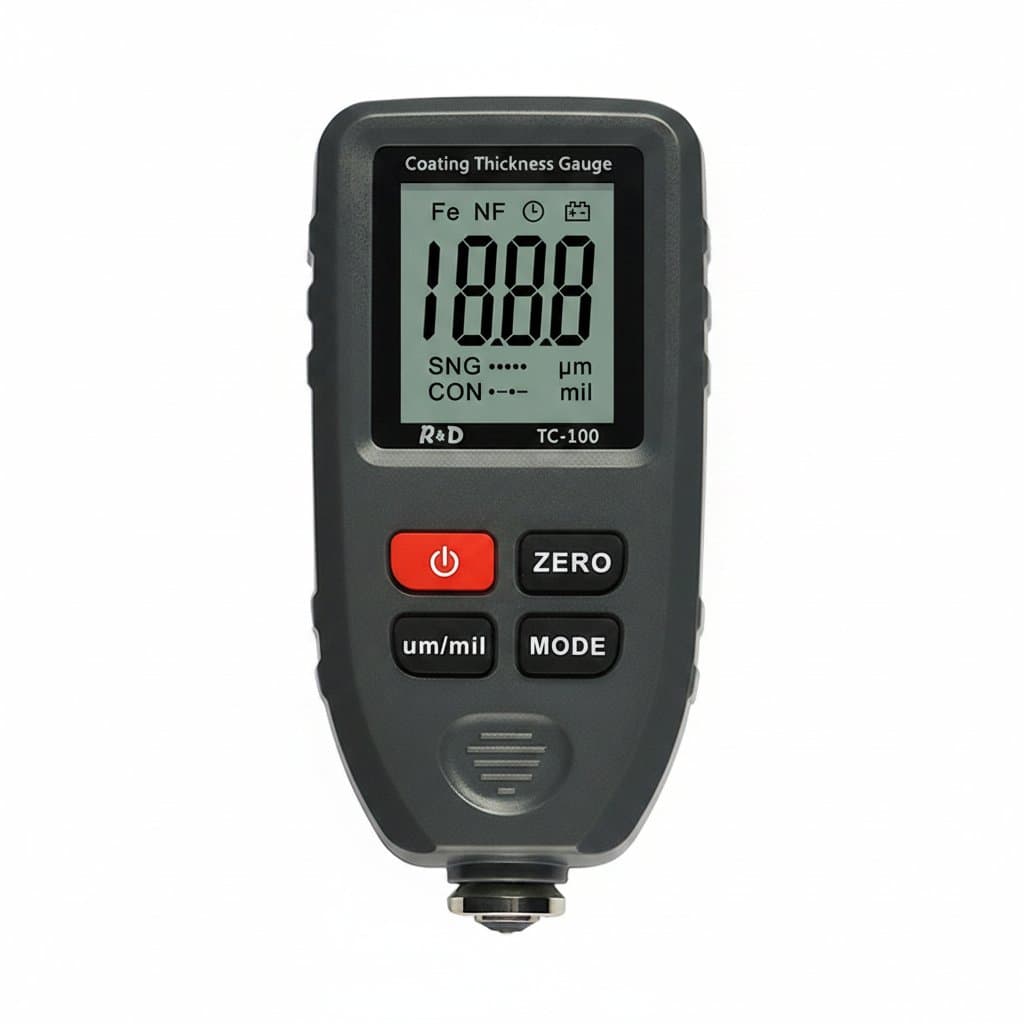
Most modern gauges are dual Fe and NFe and detect the substrate automatically, which is what you want on a vehicle with steel panels and aluminium bonnet and doors. A single mode gauge used on the wrong substrate does not give a wrong number so much as no sensible number at all, and on plastic panels neither mode works because there is nothing conductive underneath to sense.
| Substrate | Mode | Works? |
|---|---|---|
| Steel panel | Fe, magnetic induction | Yes |
| Aluminium panel | NFe, eddy current | Yes, on a dual mode gauge |
| Galvanised steel | Fe | Yes, reads zinc plus paint together |
| Plastic bumper or trim | Neither | No conductive substrate to measure against |
What a number actually means on a car
Factory paint on a modern car is a stack of primer, basecoat and clearcoat, and its total thickness is fairly consistent across a panel and between panels on the same vehicle. That consistency is the point: what you are really looking for is variation, not an absolute figure.
A panel reading much higher than the rest of the car has more material on it, which usually means a respray on top of the original, or filler underneath. A panel reading much lower can mean paint has been flatted back hard during a repair. Either way the interesting result is the outlier rather than the number.
So take many readings, not one. Work across each panel and around the car, note what the consistent baseline is for that vehicle, and treat departures from it as the finding. A single reading in isolation tells you very little, because manufacturers, colours and even panels on the same car differ.
Probe contact, curvature and calibration
The probe has to sit flat and square on the surface. Held at an angle it reads high, because part of the probe face is further from the metal than it should be. On a curved panel, a body line or a swage, the same problem appears even with careful technique, so take readings on flat areas wherever the panel allows.
The surface must be clean. Wax, polish, road film and even a heavy layer of dust add to the measured thickness, and a gauge cannot distinguish contamination from coating. Wipe the spot before measuring anything you intend to draw a conclusion from.
Calibrate against the zero plate and shims supplied with the gauge, on the substrate type you are about to measure. Calibration drifts with temperature and with probe wear, and a gauge that has been in a cold van and brought into a warm workshop is worth re-zeroing before use.
Beyond vehicles: coatings that have a specification
The same instrument does industrial work, and there the number matters absolutely rather than comparatively. Protective coatings on steelwork are specified as a dry film thickness, and both too little and too much are failures: too little does not protect for the design life, too much can crack or lose adhesion.
Galvanised steel is a case worth understanding. An Fe gauge measures everything non-magnetic between the probe and the steel, so on a painted galvanised section it reads the zinc and the paint together as one figure. Separating them means measuring before and after painting.
Where a coating specification has to be demonstrated rather than estimated, the number of readings and how they are averaged is usually part of the specification itself. A handheld gauge is the right instrument for that; a single reading quoted without the method behind it is not evidence of anything.